BMA Hay Point – Sustaining Shutdown Works

Continuing our working relationship with BMA at Hay Point, we were again engaged to provide marine assistance for a critical shutdown on one of their shiploaders. These works had us working alongside BMA and its nominated Head Contractor.

This project required the services of our marine equipment and specialist personnel to assist with the planned works that would be carried out during a 12 week outage. The planned works would see a range of maintenance activities completed on the shiploader to ensure it continues to operate reliably and safely.

As with all marine based works, this Project brought with it the need for our crew to continually adapt to the ever-changing weather conditions and modifications to schedule. By working closely with BMA and its Head Contractor, we were able to stay ahead of the game and address any hurdles in a safe and timely manner.

For these works, we provided the following specialist equipment together with expert operators:

  • 1 x self-elevating platform with 120t crawler crane
  • 1 x self-elevating platform with 250t crawler crane
  • 1 x flat top barge
  • 2 x tugs
  • 1 x work boat
  • 1 x crew boat

BMA Goonyella – Horizontal Belt Filter

Continuing our ongoing relationship, we were engaged by BMA to carry out the installation of Horizontal Belt Filter BF703 at its Goonyella mine in Central Queensland. It was our first time working back at the Goonyella mine in recent years and it was a great opportunity for our team to demonstrate our capabilities working alongside a new client team.

Our works for this project included the full turnkey package. We worked alongside BMA to assist with the procurement of key items such as pumps, drives, handrail, grating, valves, pipework and other miscellaneous componentry. We also looked after the fabrication of plate and structural steelwork packages, which were integral to the installation of the new Horizontal Belt Filter being supplied by BMA. This project once again gave us the opportunity to work alongside our trusted subcontractors for the civil, electrical and instrumentation works. Once commissioned, the upgrade would see an increase in the recovery of dry product through the mine.

The project was completed safely and on time, demonstrating our capabilities in this field and establishing our presence as a key contractor for further works at Goonyella moving forward.

BMA Hay Point – Trestle Deconstruction

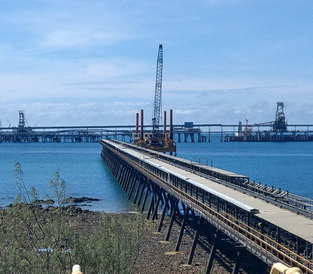
Based on our successful track record on multiple projects at Hay Point terminal, we were engaged by BMA to deconstruct and remove the original trestle and the 17BP conveyor installed when the facility opened in 1971. The ageing 1.8km structure transported coal from the terminal to waiting bulk carriers for more than 40 years and was decommissioned late in 2016.

Working from jack-up barges, our crews are dismantling the trestle and conveyor in sections, and transferring approximately 6,500 tonnes of steel to Half Tide Harbour by barge. Our work at Hay Point is ensuring that aging infrastructure is safely and carefully removed in order to best protect the local environment. In March 2019, Walz Group achieved two years recordable injury free on the project.

In conjunction with the main work of dismantling the trestle, Walz Group is undertaking additional separable portions of work under the same contract. Each separable portion of work is outlined below.

Disposal of Waste Material

Once on-shore, the trestle sections are separated into steel, concrete and timber components and prepared for transport to recycling facilities.

Dewatering and Processing of Pile Water

If the water located in the piles is not inert or has the potential to cause visual pollution, Walz is responsible for processing and filtering the water prior to release off-site.

TT8 Top Deck Removal

We are removing and disposing of the existing TT8 top deck, and installing the new structure and supporting componentry.

Berth 1 to MD2 Footbridge Installation

We have been contracted to install a new footbridge (Footbridge 2), with associated structural support and access walkways. The new structure will connect Berth 1 to MD2 after the deconstruction of 17BP conveyor and roadway.

Berth 2 Shutdown Works

The current shiploader infrastructure requires upgrading and refurbishment, as well as installation of new elements. We have completed:

  • Fender maintenance and chain replacements
  • Installation of a new davit crane
  • Upgrading the ship access gangway and supporting structures
  • Removal of redundant fenders
  • Other miscellaneous works as required

Berth 1 Shutdown Works

This refurbishment work is similar in nature to that outline for Berth 2 above and incorporates:

  • Fabrication and installation of a new tripper
  • Installation of new transfer chute and upgraded pulleys
  • Repair and surface protection to conveyor structure and rail girders
  • Supply and installation of new tripper rail
  • Installation of new walkways between berthing dolphins
  • Installation of new top Davit Crane
  • Fender chain replacements

Newcrest – Automated Ball Feeder

With a history of successful collaboration at the Lihir gold mine, working on the repair of HFO storage tanks TK01 and TK02, we were pleased to partner with Newcrest again for these improvement works to the mine’s gold processing plant. Walz was engaged to carry out the SMP and Electrical and Instrumentation works associated with upgrading three of the automated feeders on the existing ball mills at the plant.

Our scope included installation of structural steel and mechanical components (storage bin, air multipliers, feed tubes, hoists, magnets, discharge hoppers, feed launders and head box). We also performed the associated piping works required to upgrade the ball feeders. The Electrical and Instrumentation works were carried out by a specialist contractor from Australia, selected and engaged by us. We mobilised some of our plant and equipment to Lihir from Gladstone to assist with these works.

Having carried out several projects in Lihir, we recognise the importance of community engagement and always seek to engage local labour hire and subcontractors whenever we work on the island.

Sedgman – Sonoma High Cut / Low Cut

Located 6km south of Collinsville in Queensland’s Bowen Basin, QCoal Group’s Sonoma Mine produces up to 4Mtpa of hard coking and thermal coal products. 

Our client, Sedgman, has operated the Sonoma plant since it was constructed in 2007, and were seeking support for the detailed design, engineering, procurement, and construction of the High Cut Low Cut Brownfield Upgrade of the coal handling and preparation plant. We worked with Sedgman to provide SMP civil works and a range of fabrication and protective coating services. Steel fabrication included steelwork, grating, floor plate, handrails, girts, cladding and a range of process platework. We also managed civil works carried out by one of Walz Group’s trusted subcontractors.

Mechanical works included installation of cyclones, coarse coal centrifuges, product screens, conveyor idler replacements, jib crane, and various pumps and drives.

Additional works comprised miscellaneous concreting, demolition of existing structures, and the construction of various ground slabs, suspended slabs and equipment plinths.

Curragh – CPP1 Tailings Retreat Circuit

After working together successfully on previous projects, Wesfarmers Curragh Pty Ltd (WCPL) engaged Walz Group to support the installation of a new tailings retreat circuit to the Coal Preparation Plant 1 (CPP1) at its Blackwater mine in Queensland. We’ve worked at Curragh before and have gained a solid understanding of the mine’s operational requirements. For this upgrade project, we performed all structural, mechanical and piping, and electrical installation components. We outsourced the electrical works component to a trusted subcontractor. Our fabrication workshop in Gladstone produced the custom pipework, handrails, and platework for the project. Blasting and painting was also performed by Walz in our purpose built facility.

After commissioning, the upgrade increased the plant’s yield by around two percent, delivering approximately 30 tonnes per hour of additional secondary product.

The works incorporated three main areas of the tailings retreat circuit — the Eastern building, the Western building and the secondary product conveyor. A new clarified water pump was also installed to supply the additional demand from the new circuit.

Connecting to the eastern side of CPP1, the Eastern building houses the tailings cyclones, sieve bends, spirals feed sump, and the relocated spirals feed pump.

The Western building connects to a previously existing structure and incorporates the spiral banks, spirals product sump and pump, spirals product cyclone cluster, fine coal centrifuge, and the reject sump and pump.

The secondary product conveyor is fed by the centrifuge, running from the new Western building to transfer product onto the existing steaming coal conveyor.

Newcrest – Tank TK201 Repair

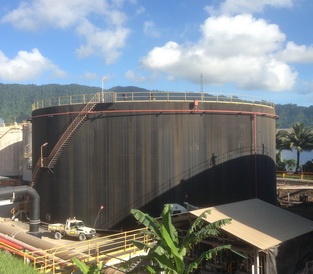
On the strength of previous work performed for Newcrest at their Lihir Gold Mine — particularly the works carried out on Heavy Fuel Oil (HFO) tank TK202 — Walz Group was engaged to conduct a 10 year statutory inspection on HFO tank TK201.The scope included undertaking all repairs found necessary as a result of the inspection.

Similar to the TK202 works carried out in 2017, Walz identified numerous repairs and upgrades that were required to ensure the tank maintained its compliance. These works included:

  • Removal and replacement of roof components (inner rafters, annular ring, braces, roof plates, manway and miscellaneous cleats and beams)
  • Replacement of top strakes
  • Repair of external stairway
  • Replacement of all handrail and kickplate around the top of the tank
  • Replacement of goose neck vent on the roof nozzle
  • Remove and replacement of existing fire water ring main risers and circumferential pipework
  • Full blast and repaint of the inside of the tank shell and roof prior to hydro test
  • Hydro testing of the tank

Cement Australia – Heat Exchanger Duct Replacement

Cement Australia’s operations in Gladstone incorporate Australia’s largest cement kiln, capable of producing more than 1.6Mtpa of cement.

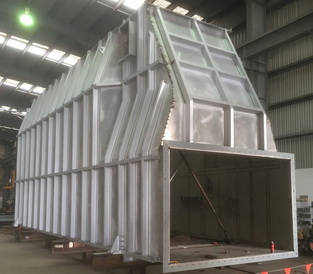
Early in 2017, it was identified that the heat exchanger duct between the clinker cooler and the inlet to heat exchanger no.1 (HE1) had reached the end of its life, and was significantly impacting on plant production. Cement Australia engaged Walz Group to replace the equipment to return the kiln performance to full capacity. The project required us to remove and replace the failing heat exchanger, ductwork, inlet chamber, associated supports, and specified tubes during a time critical shutdown.

We utilised our dedicated fabrication facility to manufacture all the ductwork, inlet chamber, and the associated supports and components. We also applied protective coating as required. Prior to the shutdown for the replacement works, we reinforced the plant foundation and structure to ensure it could accommodate additional loads.

Our comprehensive plant and equipment fleet was invaluable for this project, which required craneage and scaffolding to remove and replace the existing structure.

Newcrest – Tank TK202 Repair

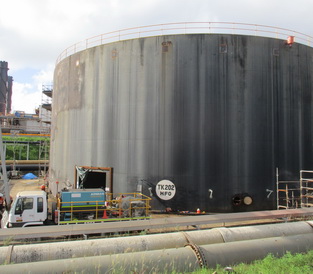
Newcrest Mining Limited (formerly Lihir Gold Limited) operates a gold mine and processing facility on Lihir Island in Papua New Guinea. Two Heavy Fuel Oil (HFO) storage tanks (TK201 & 202) were constructed for the original plant in 1996 and one new IPS HFO storage tank was later commissioned in 2013. TK201 and 202 were originally designed and constructed to API 650 for a nominal storage capacity of 14,000l each.

Following maintenance inspections on TK202 in 2009 and later in 2012, Newcrest identified various repairs and upgrades required to ensure the tank maintained its compliance. Walz Group was engaged to assist with this scope of works which included:

  • Internal inspection of the tank
  • Repairs to the tank’s annular ring, shell, roof and tank furnishings
  • Repairs to the tank’s internals including floor, support columns and roof framing
  • Repairs to protective coatings

BMA Hay Point – Stacker Reclaimer SR1 & SR2 Refurbishment

When the existing stacker-reclaimer stockyard machines (SR1 and SR2) at the Hay Point coal terminal started to approach the end of their life, BMA commenced the process of replacing them. With an anticipated lead time of two years for the new equipment to be manufactured and shipped to Australia, the machines needed work to be kept operational until the replacements arrived.

Walz Group was contracted to dismantle both stacker-reclaimers down to the fixed cone to undertake structural integrity repairs. This would extend the life of both machines for the interim lead time of their replacements. The works involved removal of mast, pendants, bucket wheel boom, counterweight arm, counterweight box and slew cone.

The machines were then rebuilt with new slew cone, new counterweight assembly and refurbished bucket wheel boom. Both machines were jacked up to clear the rails to remove all bogies, which had to be refurbished and machined to suit the new rail profile.

Our fabrication workshop and protective coatings workshops Gladstone were instrumental in the repair and refurbishment of existing componentry.